Limbă

Every coil of wire that enters a forming shop carries a decision with it: is this part better made on a cam-driven spring machine, a dedicated coiler, or a CNC wire forming machine? The short answer for most modern production lines is the CNC wire forming machine, because it converts shape changes into software changes rather than toolroom changes. Once the program is stored, the same machine can move from a simple hook to a multi-bend three-dimensional bracket in roughly the time it takes to load a new file.
This guide explains what a CNC wire forming machine actually does, how its axis configuration changes capability, where it overlaps with spring coilers, and what to verify before you commit capital to one. The conclusion up front: if your part mix includes torsion springs, wire clips, hooks, brackets, or any geometry that bends in more than one plane, this machine class offers the widest usable range per dollar of any wire-forming equipment.
The capability boundary of a CNC wire forming machine is wider than many buyers assume. It is not limited to helical springs, although it can produce many spring families. The machine's real strength is creating shapes from wire that require bending in different directions, forming loops at the ends, twisting legs, and cutting off cleanly. Compared with a mechanical cam machine, the CNC version removes the time and cost of designing, cutting, and proving cams for each new part.
There is one important boundary. If you need a single compression spring design in very high volume for months at a time, a dedicated CNC spring coiling machine will usually produce it faster. CNC wire forming machines earn their position when part variety is high and changeovers are frequent, which is the normal condition in contract manufacturing and OEM supply shops.
All CNC wire forming machines follow the same sequence: straighten, feed, bend, cut. The differences between models come down to how many bending axes act on the wire simultaneously, how precisely the feed length is controlled, and how quickly the control system recalculates tool positions for a new part program.
From a workflow standpoint, every bend, feed length, and cut position is defined in the controller as a coordinate value. That is what makes changeover fast: you do not physically modify the shape-generation system beyond changing the guide and tooling block. The same logic also makes automatic correction possible, because the control system can compare commanded positions with actual feedback from each servo axis.
Axis count is the most quoted specification in wire forming because it correlates with the complexity of the geometry you can build in one pass. As a rule, do not buy more axes than your product roadmap justifies; a 10-axis machine costs more to operate, program, and maintain than a 3-axis machine. At the same time, if you accept work with multi-plane bends, under-specifying leads to slower cycles, manual secondary operations, and inconsistent part quality.
| Axes | Forming Freedom | Typical Parts | Typical Wire Range |
|---|---|---|---|
| 3-axis | Feed, horizontal bending, cut | Hooks, simple clips, small extension springs | 0.3 to 3.0 mm |
| 5-axis | Adds tool axes for off-plane movement | Torsion springs, 3D clips, small automotive brackets | 0.5 to 5.0 mm |
| 6/7-axis | More simultaneous tool positions | Multi-bend 3D forms with tight radii | 1.0 to 6.0 mm |
| 10-axis | Two forming arms with multi-tool control | Complex 3D springs and formed assemblies | 1.5 to 10.0 mm |
| 12-axis camless | Maximum tool mobility, no cams | Complex medical, aerospace, and high-mix parts | 0.5 to 12.0 mm |
A 3-axis machine is the lowest-cost entry point and remains the most popular configuration for shops whose parts are flat hooks, clips, and simple springs. When your engineers start designing torsion springs with offset legs or wire forms that bend in two planes, the jump to a 5-axis machine removes most of the tooling compromises. 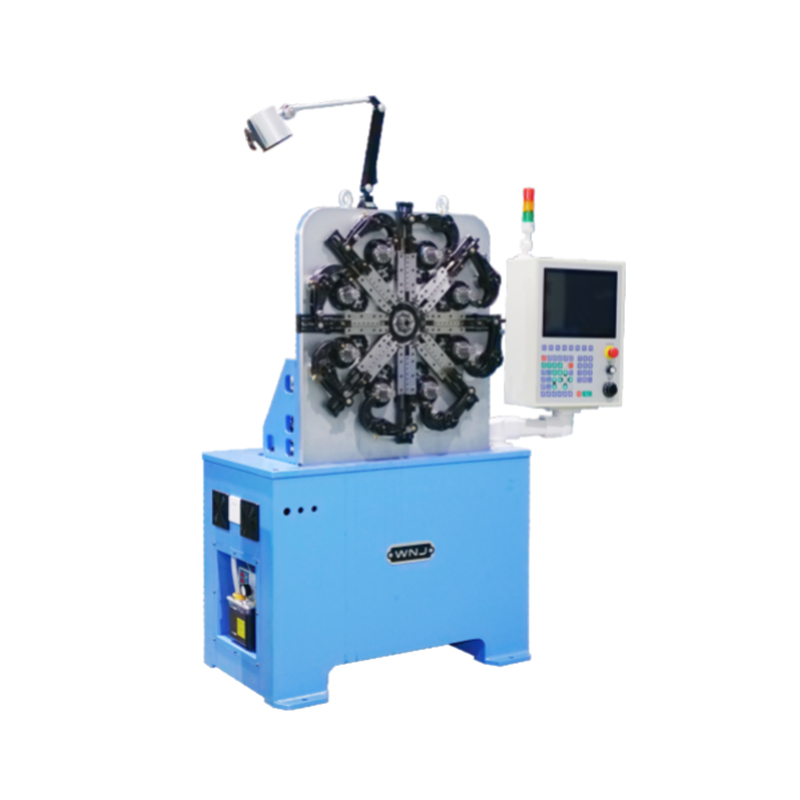 CNC-625D 3-Axis Spring Forming Machine for Simple SpringsThis 3-axis forming machine offers the lowest entry cost for shops producing flat hooks, clips, and simple springs. Its four-axis control enables single-step or synchronous operation with automatic stop for defective parts.View Product →For reference, the 625D-class 3-axis forming machine in the WNJ lineup covers this segment, while the 625Z/635Z/650Z series extends the same forming principle to five controlled axes.
For shops that quote mixed production runs, the 10-axis and 12-axis camless configurations provide the widest operating envelope. Their advantage is simultaneous movement of multiple tool carriers, which reduces cycle time on parts that would otherwise need indexing or repositioning. The trade-off is a steeper programming requirement and a higher purchase price.
People frequently use the two terms interchangeably, but they refer to different strengths. A CNC spring coiling machine is optimized for helical shapes at high speed, while a CNC wire forming machine is optimized for arbitrary 3D wire shapes and spring types that need bending rather than wrapping. The correct choice depends on your dominant part geometry, not on the machine brand or price alone.
Many spring production lines keep both machine types side by side. If you expect one wire forming machine to replace a coiler for straight compression work, compare the real cycle times on your own wire diameter before committing. For parts that combine helical sections with legs and bends, a wire forming machine with a mandrel accessory can often consolidate what would otherwise require two machines. When the part is primarily a bent wire form rather than a helix, a 4-axis wire bending machine is the more targeted option. 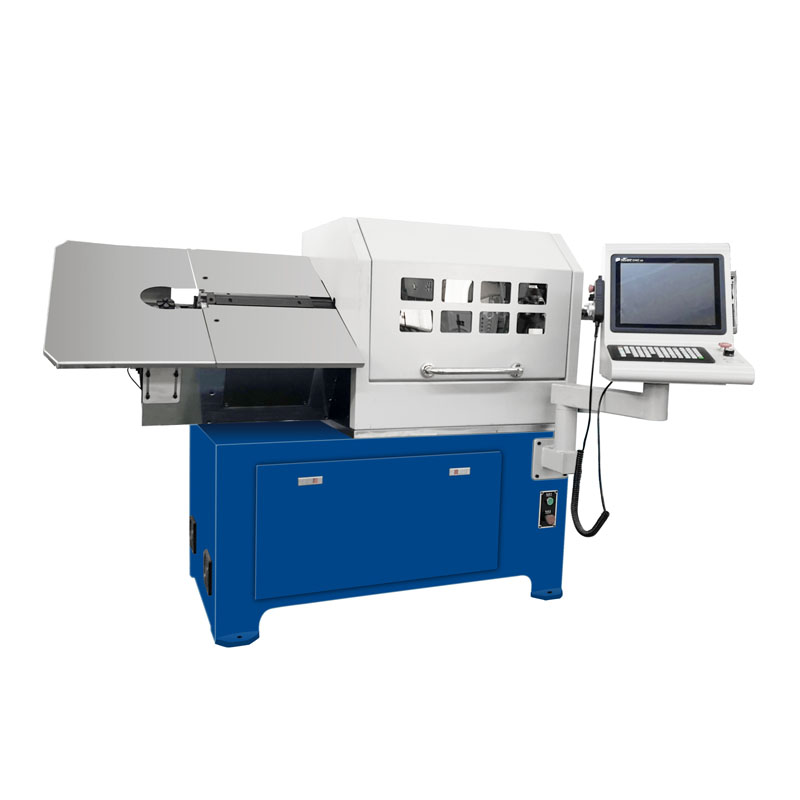 ZW-480 4-Axis CNC Wire Bending Machine for Bent Wire FormsWhen your part is primarily a bent wire form rather than a helix, this 4-axis bending machine provides targeted efficiency. Its four/seven axes linkage design ensures high precision and stable performance across diverse wire bending applications.View Product →
CNC wire forming machines are not confined to spring manufacturers. The same bending and cutting logic shows up in almost every engineered product that contains a formed wire component. The application pages on the WNJ site identify eight verticals where this equipment is used daily:
The common thread is dimensional consistency. In automotive production, for example, a seat spring that drifts by one millimeter in its leg angle can create noise and premature wear in the final assembly. A five-axis machine holds the tool path with enough repeatability that every part coming off the line matches the approved sample. 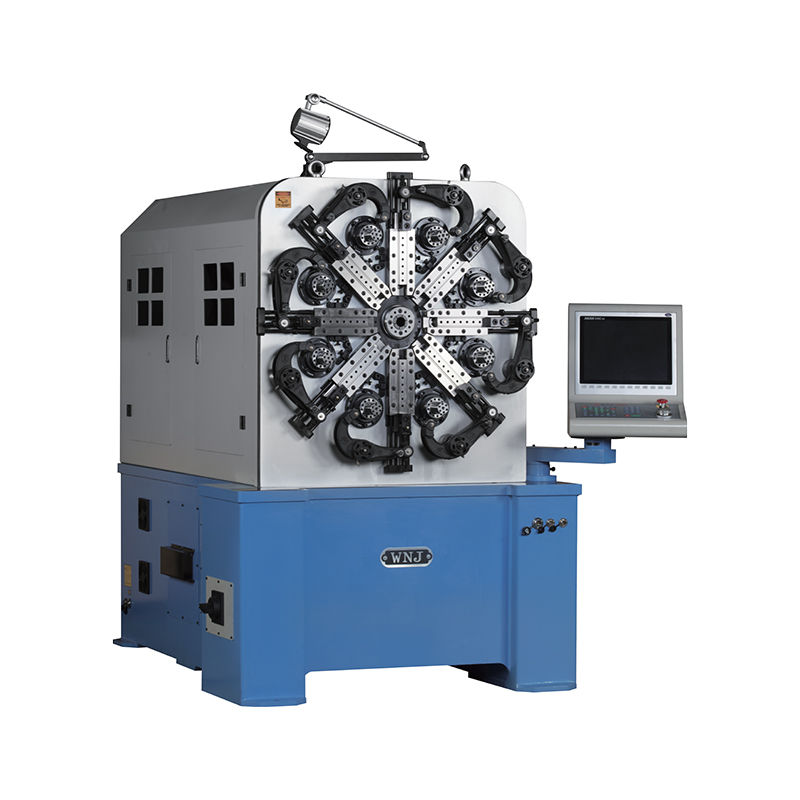 CNC-635Z 5-Axis Spring Forming Machine for Consistent Dimensional AccuracyThis five-axis forming machine delivers the repeatability required for automotive seat springs and similar precision parts. The rotary wire feeding mechanism eases setup, while five-axis control maintains tight tolerances on leg angles and diameters.View Product →That is why manufacturers in these industries ask for trial parts made from their own material before they approve a machine.
Before you compare price tags, compare these seven factors. A machine that is 5 percent cheaper can cost 20 percent more in tooling and downtime if the specification does not match your wire diameter and tolerance requirements.
These points are covered in practical detail in our guide on how to choose the correct spring machine. The summary is simple: let your part family define the specification, then use trial parts to validate the real behavior before purchase.
The accuracy of a CNC wire forming machine is the result of mechanical condition as much as software. Clean guides, aligned rollers, and correctly tensioned feed systems keep tolerances repeatable through thousands of cycles. The daily routine is short, but skipping it leads to drift that appears only in final inspection.
Operators should also understand the machine's normal sound and vibration signature. Unusual noise from the feed section or a sudden change in bend angle usually appears before a complete failure, and early action avoids longer downtime.
CNC spring machine is a broad term that usually covers both coilers and forming machines. In practice, a spring coiling machine is optimized for helical springs, while a wire forming machine produces bent wire shapes, torsion springs, extension springs, and other non-helical geometries. Most factories use both to cover the full product range.
Common materials include carbon spring steel, stainless steel grades such as 302, 304, and 316, phosphor bronze, beryllium copper, aluminum, and various coated wires. The two key limits are the machine's wire diameter range and the maximum tensile strength that the feeding and straightening system can handle. If you plan to run hard-drawn wire above 2000 MPa, check the straightener roll material and the feed roller pressure range before purchase.
If most parts are single-plane clips and hooks, a 3-axis machine is sufficient. Torsion springs with offset legs benefit from 5-axis control. Multi-plane 3D wire forms typically need 6 axes or more. A practical rule is to choose one level above your current average complexity so you can accept a wider range of jobs without buying a second machine.
Yes, within limits. Compression springs with closed ends and tight pitch are the strong domain of a coiler, but a wire forming machine equipped with a pitch tool and mandrel can produce compression springs efficiently at moderate speeds. It is especially attractive in small batches where changeover time matters more than maximum cycle speed.
For a simple geometry change within the same wire diameter, tooling adjustments typically take 15 to 40 minutes plus program selection. If the wire diameter changes, you also change guides, feed rollers, and forming tools, which usually takes one to two hours on most machines. A cam-driven alternative would require cutting and proving new cams, which takes considerably longer.
Practical repeatability is usually in the range of plus or minus 0.5 to 1 degree for bend angles and plus or minus 0.1 mm for lengths, depending on wire diameter, spring-back behavior, and material consistency. Always confirm these figures with a trial run using your actual wire, because material spring-back has the largest influence on final geometry.
The right choice always comes back to your part family, not the machine nameplate. If your product mix includes varied wire forms and spring geometries, a CNC wire forming machine remains the single piece of equipment with the widest usable range. Verify the axis count, check the wire diameter coverage, confirm the support network, and ask for trial parts made from your material before you sign. That process takes a few days, but it protects the machine investment for a decade or more.
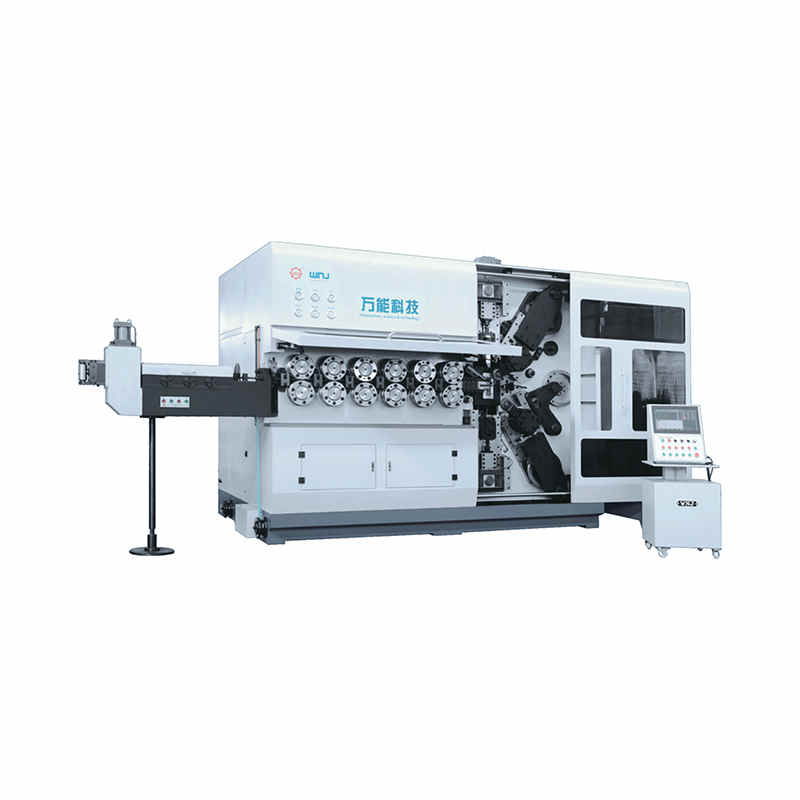
TK-13200, TK-7230 TK-13200、 TK-7230 MAȘINĂ CNC DE BOBINARĂ A ARCOLOR 12 AXE ...
Vezi detalii
TK-13200, TK-7230 TK-13200、 TK-7230 MAȘINĂ CNC DE BOBINARĂ A ARCOLOR 12 AXE ...
Vezi detalii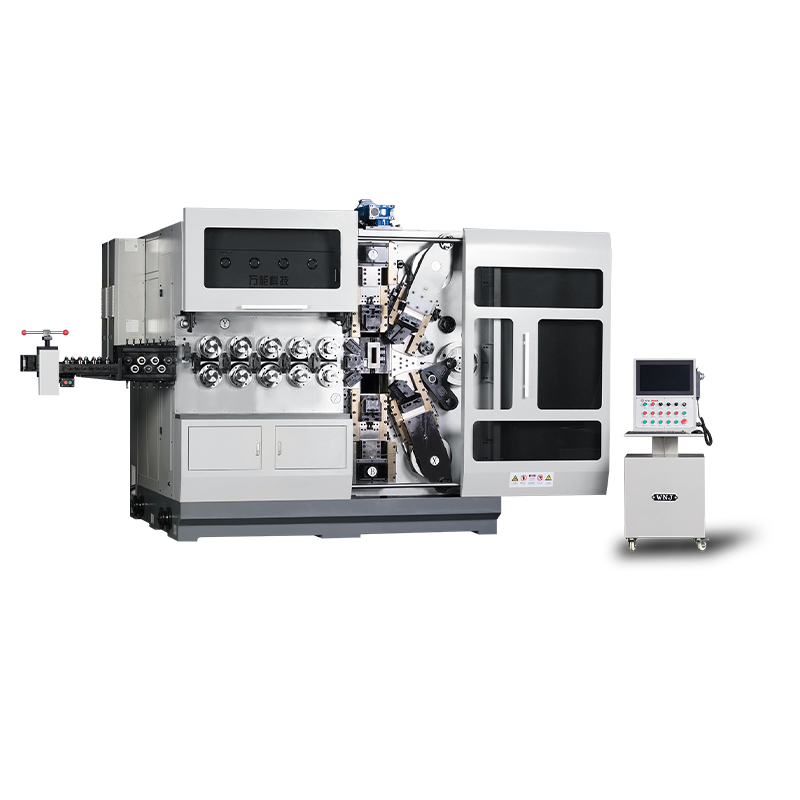
TK12120 TK-12120 MAȘINĂ CNC DE BOBINARĂ A ARCOLOR 12 AXES ...
Vezi detalii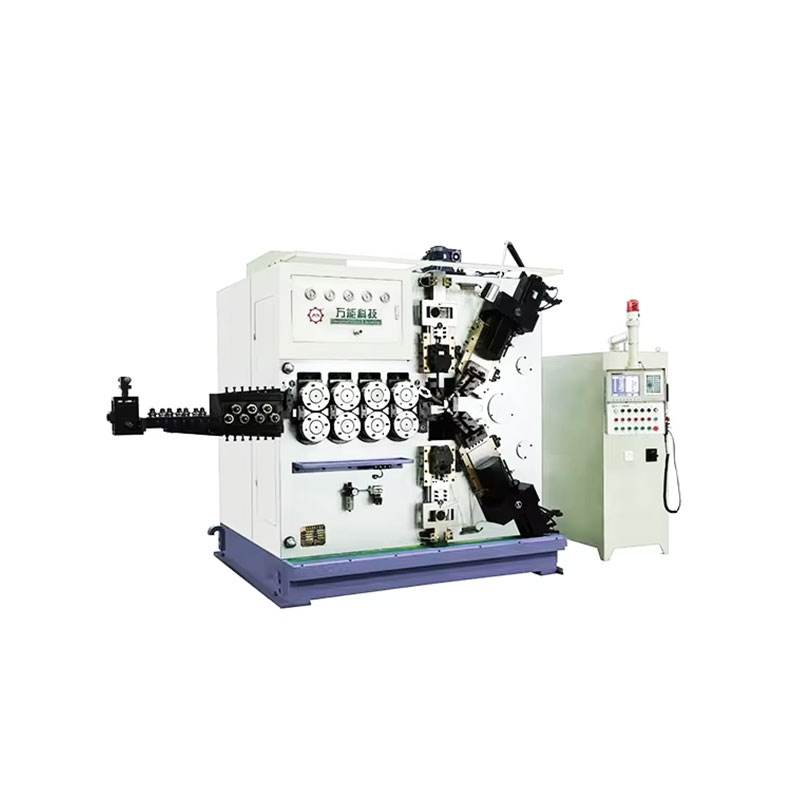
TK-6160 TK-6160 MAȘINĂ CNC DE LAMINARE A ARCOLOR ...
Vezi detalii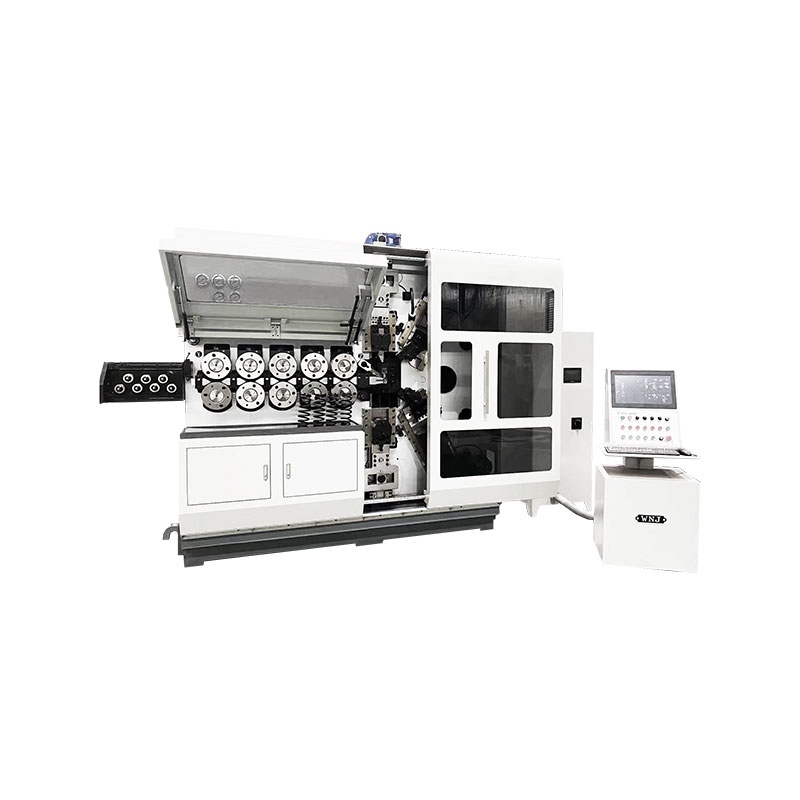
TK-6120 TK-6120 MAȘINĂ CNC DE LAMINARE A ARCOLOR ...
Vezi detalii
TK-5200 TK-5200 MAȘINĂ CNC DE BOBINARĂ A ARCOLOR 5 AXE ...
Vezi detalii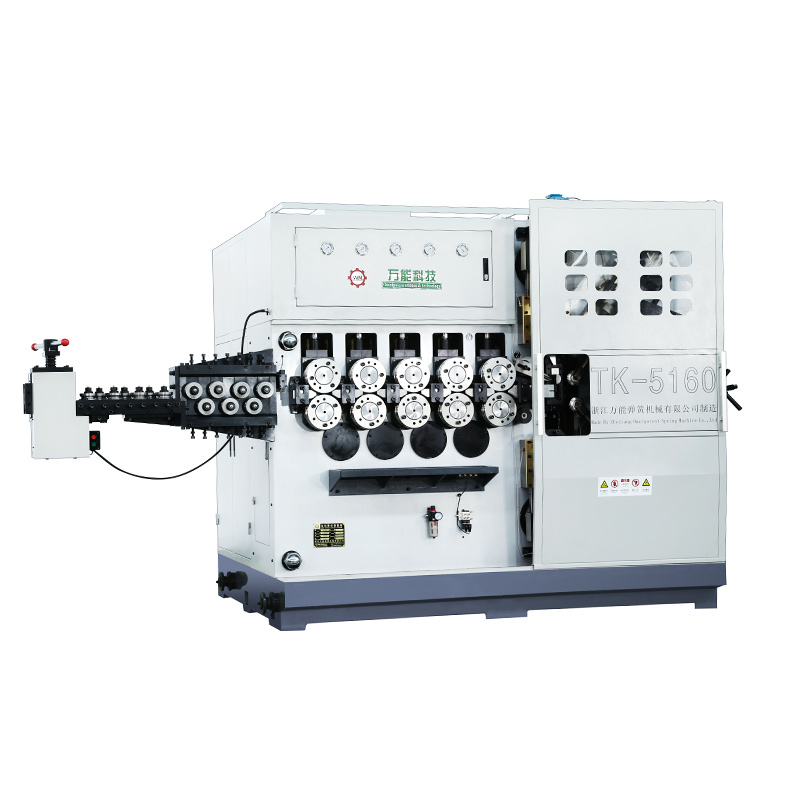
TK-5160 TK-5160 MAȘINĂ CNC DE BOBINARĂ A ARCOLOR 5 AXES ...
Vezi detalii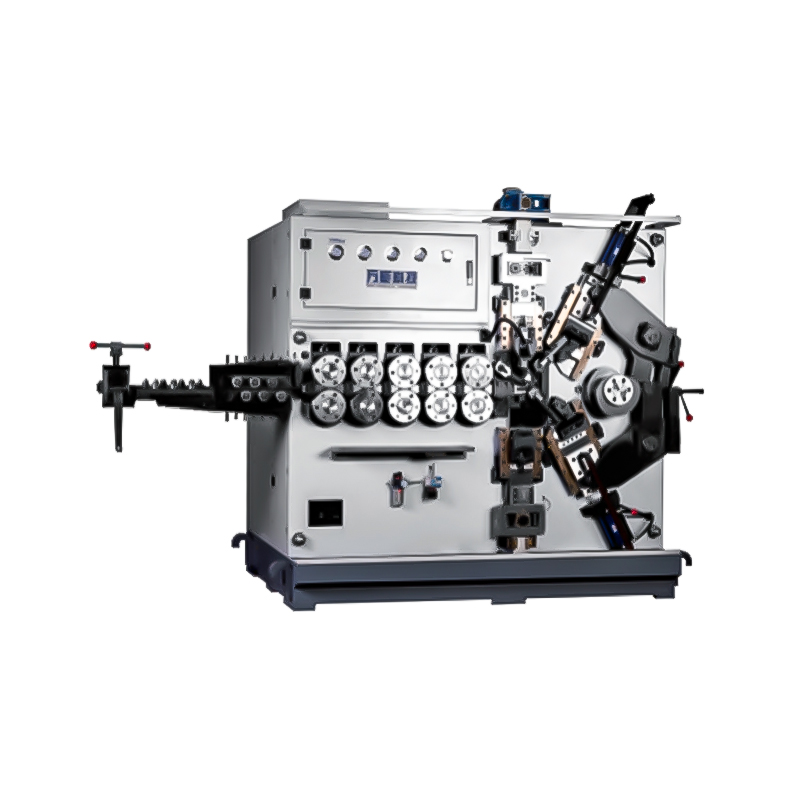
TK-5120 TK-5120 MAȘINĂ CNC DE BOBINAR A ARCOLOR 5 AXE ...
Vezi detaliiCod QR mobil